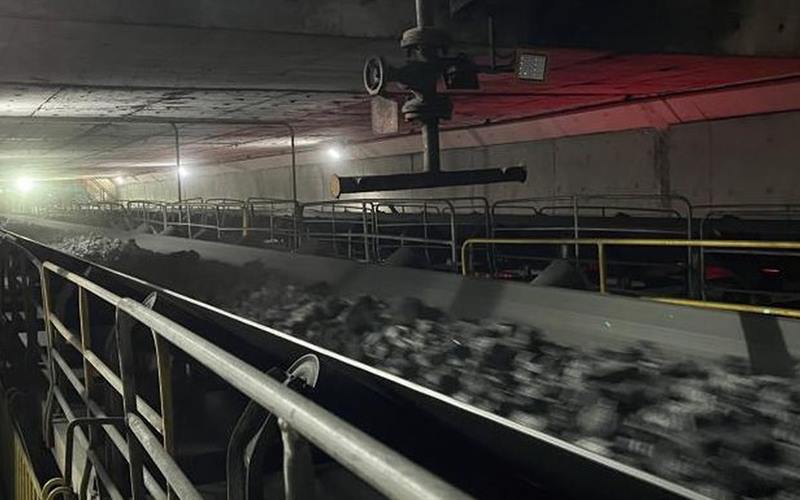
Safety critical conveying
Fire resistant belts
Zero Ignition, Total Control: Bulker Belting Solutions engineers the ultimate line of defense for high-risk extraction environments: our premium Fire-Resistant Mining Belts. In enclosed processing facilities, above-ground handling yards, and underground tunnels, conveyor friction or external sparks can trigger devastating fires. Our belts are chemically weaponized with advanced self-extinguishing rubber matrices designed to choke out flames instantly, eliminate toxic smoke propagation, and protect both your personnel and your high-value infrastructure.
When safety guidelines and mine compliance leave absolutely zero room for compromise, Bulker Belting Solutions delivers fire-suppression performance you can trust with your life.
- Fire
- Mining and quarries
- Power and coal
- Chemicals and fertilizer
Critical Safety & Performance Engineering
- Self-Extinguishing Polymer Matrix. Formulated with specialized fire-retardant chemical additives that automatically starve the flame of oxygen the moment the ignition source is removed.
- Anti-Static Carbon Dispersion. Engineered with specialized anti-static compounds that safely dissipate dangerous electrostatic buildup, eliminating the risk of spark-induced dust explosions.
- Low-Smoke, Non-Toxic Formulations. Developed to minimize hazardous smoke density and toxic gas emissions, maximizing visibility and breathing safety during underground emergency evacuations.
- Severe Mechanical Toughness. Fire protection does not come at the expense of strength. These belts retain elite resistance against heavy gouging, deep cutting, and brutal abrasive wear from jagged ores.
- High-Strength Core Integration. Available across our entire carcass spectrum, including multi-ply fabric (EP/NN), Straight Warp, Solid Woven, and Steel Cord structural cores.
Built for High-Risk & High-Compliance Sectors
Our premium flame-retardant belts are engineered to satisfy the strictest international safety audits across critical bulk handling networks:
- Underground Coal Mining: Eliminating methane and coal-dust ignition vectors in highly volatile, confined underground faces.
- Power Generation & Biomass Facilities: Safeguarding high-speed transfer lines carrying volatile coal dust, wood pellets, and dry biomass.
- Grain & Sugar Handling Terminals: Prevent static-spark risks in highly combustible organic dust environments.
- Closed Tunneling & Enclosed Silos: Providing crucial low-smoke protection where escape routes and ventilation are physically restricted.
Global Safety & Compliance Standards
Every fire-resistant belt from Bulker Belting Solutions undergoes rigorous laboratory validation, ensuring strict compliance with the world’s leading mine safety certificates:
| Compliance Rating | Target Environment | Primary Safety Characteristic |
|---|---|---|
| MSHA (Title 30 CFR) | Underground Mine Safety (USA) | Passed rigorous laboratory flame-pipe and tunnel propagation tests |
| DIN EN 12882 | Above-Ground Industrial Use (Europe) | Comprehensive electrical conductivity (ISO 284) and drum friction safety |
| DIN EN 14973 | Underground Mining (Europe) | Maximum fire safety and non-ignition under extreme friction stalling |
| AS 1332 / ISO 340 | International Mining Standards | Self-extinguishing properties that kill flames in under 15 seconds |
Protect Your Crew, Safeguard Your Infrastructure
In high-risk mining and bulk handling, a single spark can cause a catastrophic facility shutdown or threaten human life. Bulker Belting Solutions’ fire-resistant technology acts as a permanent, built-in safety insurance policy for your entire plant footprint.
Secure full regulatory compliance and absolute peace of mind today.