Mining solutions
Conquer the Extremes with BULKER Belting Solutions
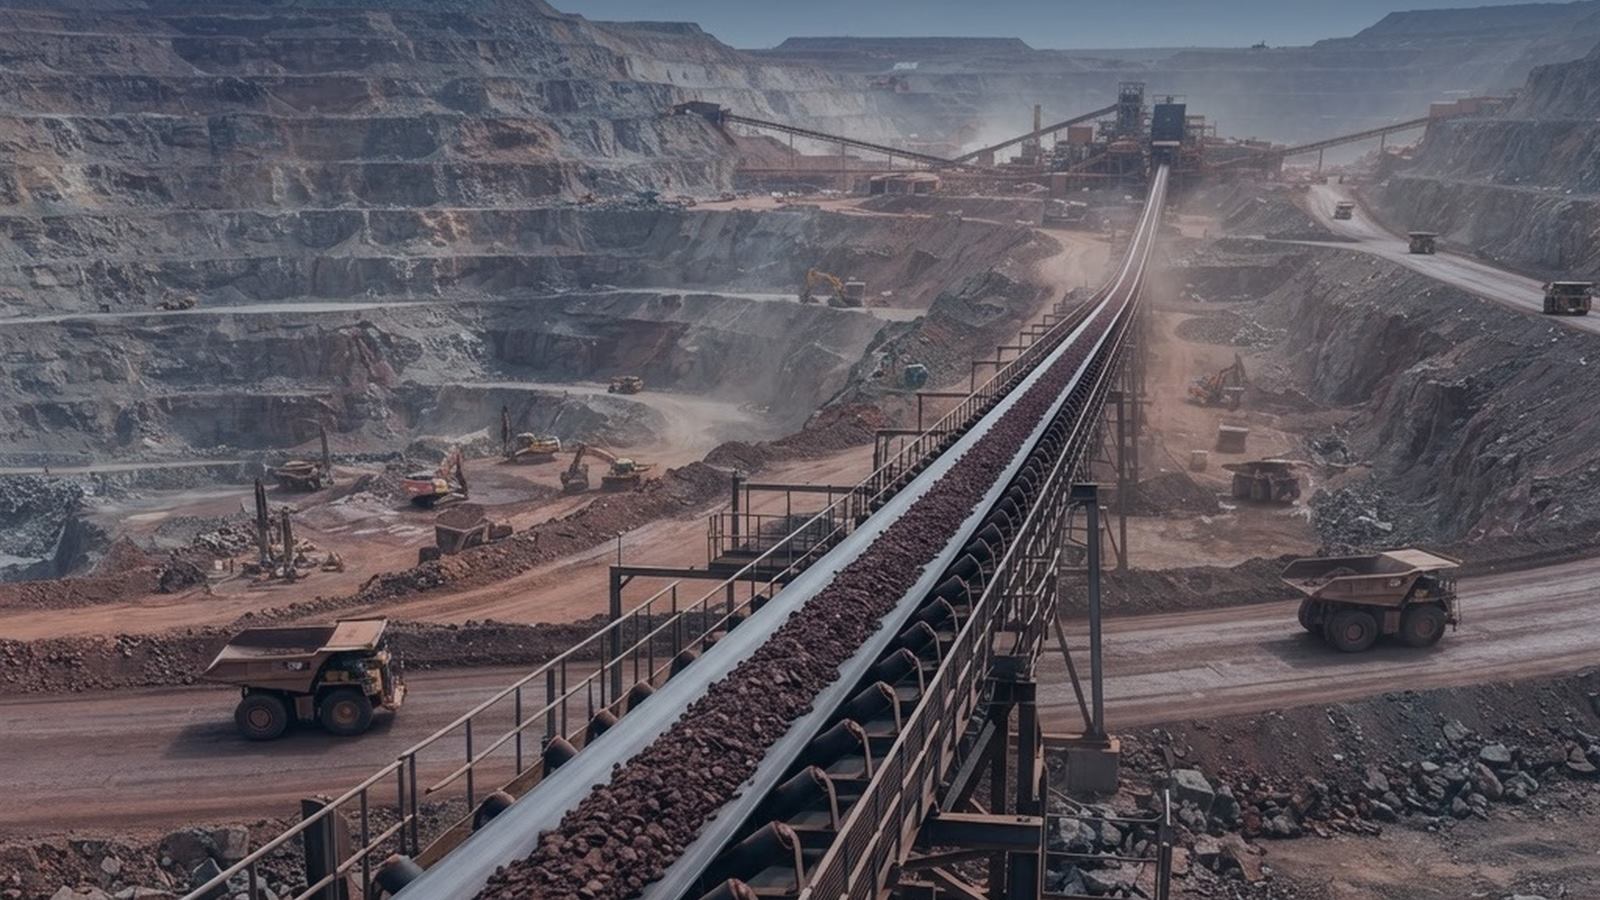
In the mining industry, your conveyor belt is your lifeline. Standard rubber breaks down, cracks, and tears when pushed to the limit, causing costly downtime. That is why BULKER Belting Solutions engineers specialized cover compounds designed to survive the harshest environments on Earth.
From deep underground coal faces to blistering surface smelters, we keep your operations moving. Discover our lineup of high-performance mining belts:
Fire-Resistant & Flame-Retardant Belts
Safety without compromise. Engineered with advanced self-extinguishing properties, these belts meet the strict legal safety standards required for underground coal mining.
Abrasion-Resistant Belts
Built for brutal impact. Crafted from heavily toughened rubber compounds, they easily withstand the constant, grinding wear of jagged granite, iron ore, and heavy rocks.
Heat-Resistant Belts
Defying the thermometer. Our premium thermal compounds are built to carry blistering materials up to 400°C directly from smelters, kilns, and ovens without cracking or melting.
Oil-Resistant Belts
Zero swelling, zero warping. Specially formulated to resist chemical degradation from lubricants and oily minerals, ensuring your belt stays perfectly tracked and structurally sound.
Cold-Resistant Belts
Arctic-grade reliability. Formulated to maintain peak flexibility and elasticity in sub-zero surface mining environments, preventing brittle snaps.
Chemical-Resistant Belts
The ultimate anti-corrosive barrier. Designed specifically to endure aggressive acidic leaching lines and wet chemical processing plants without corroding.
Have a mining project to discuss?
Contact a BULKER Belting Solutions specialist for a customized spec sheet or a quote.