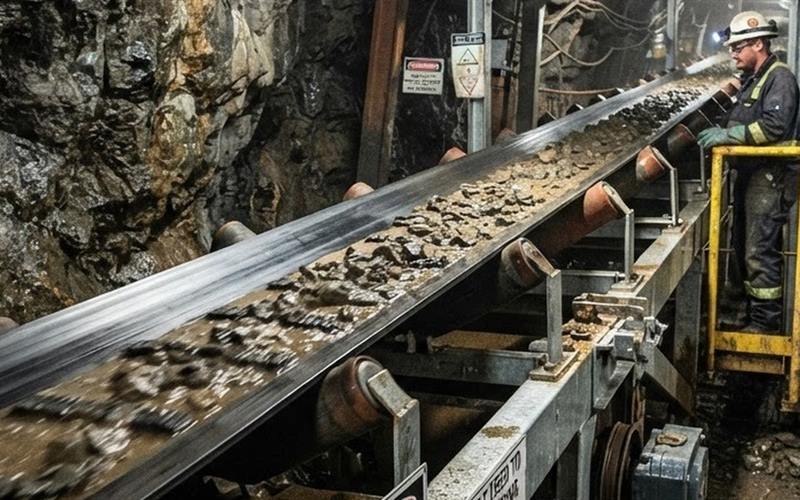
Chemical resistant
Acid-alkali resistant belts
Corrosion-Proof Bulk Handling: Bulker Belting Solutions engineers the ultimate chemical defense for aggressive industrial processing: our premium Acid & Alkali Resistant Conveyor Belts. When exposed to corrosive chemicals, fertilizers, or acidic ores, standard rubber swells, softens, and quickly dissolves, causing rapid belt degradation and catastrophic system failure. Our belts are chemically weaponized with specialized synthetic polymers designed to completely repel corrosive compounds, maintaining total structural integrity and high-tensile strength in the most volatile environments.
When your processing lines run hot with acids, bases, and corrosive salts, Bulker Belting Solutions provides an unbreachable barrier to keep your tonnage moving.
- Chemical
- Mining and quarries
- Cement
- Chemicals and fertilizer
Key Chemical Engineering Advantages
- Immune to Chemical Swelling. Formulated with highly stable synthetic polymers that block chemical absorption, completely eliminating the swelling, blistering, and peeling that ruins standard rubber.
- Corrosion-Proof Synthetic Carcass. Built with premium EP (Polyester/Nylon) or specialized fabric cores that are chemically inert, ensuring the inner skeleton of the belt never rots or loses tension from chemical leaks.
- Excellent Acid & Base Defiance. Provides elite defense against a wide spectrum of aggressive agents, including phosphoric acid, sulfuric acid, hydrochloric acid, nitric acid, and sodium hydroxide.
- High-Adhesion Integrity. Advanced cross-linking skim rubbers prevent chemical moisture from penetrating the plies, entirely eliminating the risk of internal ply separation or delamination.
- Elite Wear & Gouge Resistance. Chemical resistance does not compromise structural toughness. These belts maintain high tensile strength and abrasion resistance against heavy, jagged bulk materials.
Built for the Industry's Most Aggressive Environments
Our premium acid-alkali resistant belts are the definitive choice for chemical processing and highly corrosive material sorting lines:
- Chemical & Fertilizer Plants: Transporting raw sulfur, phosphates, potash, urea, and finished chemical compounds.
- Mineral Processing & Leaching Plants: Handling aggressively acidic or alkaline copper, gold, and nickel ores during chemical extraction phases.
- Cement & Gypsum Facilities: Managing highly alkaline industrial minerals, wet slag, and corrosive additives.
- Pulp, Paper, & Water Treatment: Transporting chemically treated wood chips, wet sludge, and corrosive processing agents.
Chemical Compatibility Overview
Every acid- and alkali-resistant belt from Bulker Belting Solutions is precisely compounded to meet specific industrial chemical hazards:
| Cover Class | Chemical Spectrum | Concentration Range | Primary Field Applications |
|---|---|---|---|
| Class A1 (Acid Dominant) | Sulfuric, Phosphoric, Hydrochloric Acids | Highly concentrated acids | Fertilizer production, chemical leaching plants |
| Class A2 (Alkali Dominant) | Sodium Hydroxide, Potassium Hydroxide | High pH alkaline solutions | Pulp mills, heavy industrial chemical plants |
| Class A3 (Universal Duty) | Moderate Acids, Alkalis, and Corrosive Salts | Standard commercial concentrations | Gypsum handling, salt mining, coal washing lines |
Neutralize Corrosion, Secure Continuous Uptime
Don't let chemical wear melt away your plant's profitability or force frequent, expensive conveyor line changeouts. Bulker Belting Solutions’ advanced chemical-resistant technology provides a bulletproof shield for your conveyor system, delivering a radically extended lifespan and lower total operational costs.
Stop chemical erosion and shield your bulk processing network today.